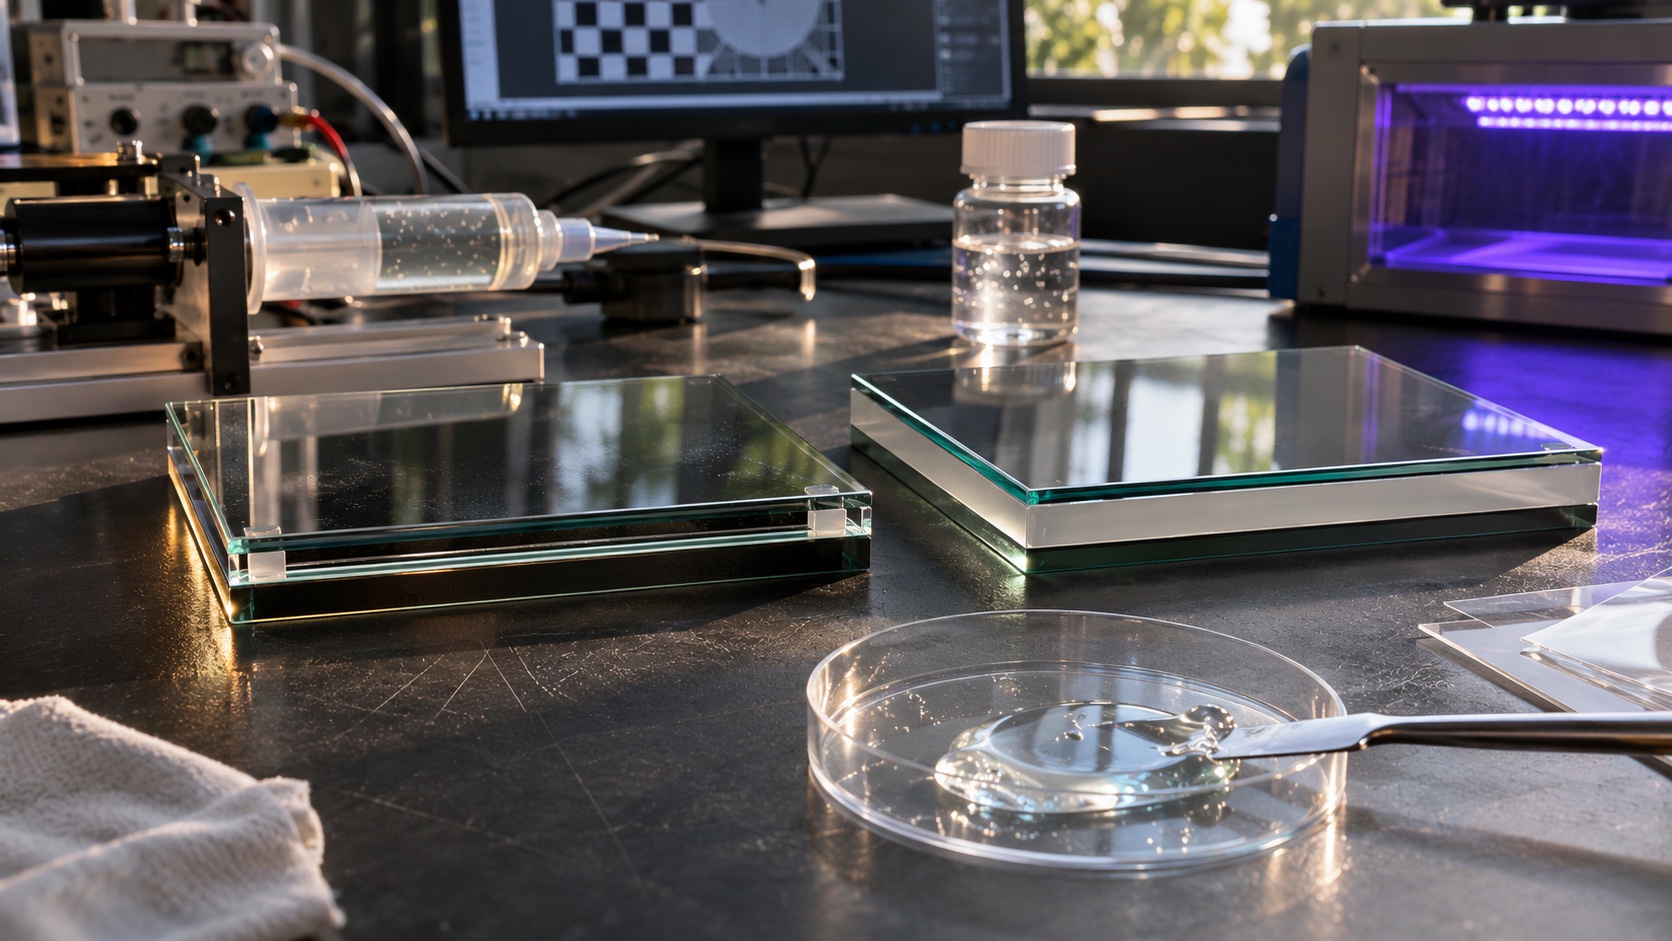
Two touch displays can use the same LCD and look different once the cover glass is installed. One shows a second reflection and washed-out blacks near a window; the other looks clearer but costs more to assemble and is harder to repair.
Optical bonding fills the space between display layers with an optically suitable adhesive. An air-gap assembly leaves a controlled separation. Choose between them using optical performance, environment, yield, serviceability, and total assembled cost.
Define which layers are being joined
A display stack may contain cover glass, a touch sensor, polarizers, the LCD, coatings, and mechanical supports. “Bonded display” can refer to different interfaces, so require a drawing that identifies each layer and adhesive.
Ask whether the touch sensor is bonded to the cover, whether that assembly is bonded to the LCD, and whether the edges are sealed. These distinctions affect reflections, moisture paths, and repair.
The adhesive must be compatible with the surfaces, panel structure, temperature range, UV exposure, and mechanical stress. Its optical clarity at room temperature is only one property.
| Criterion | Air gap | Optical bonding |
|---|---|---|
| Internal reflection | More interfaces can reflect light | Fewer air interfaces |
| Assembly process | Mechanically simpler in many designs | Requires controlled bonding and inspection |
| Dust and condensation | Gap must be protected | Bonded region removes an air cavity |
| Rework | Layers may be separable | Separation can damage parts |
| Mechanical behavior | Supports must prevent contact and flex | Bond distributes load but adds stress considerations |
| Cost | Lower process cost may be possible | Added material, process, and yield cost |
Evaluate optical performance on the final stack
The strongest benefit of bonding often appears in bright ambient light. Reducing internal reflections can improve perceived contrast without requiring the same increase in backlight power.
Measure the assembled unit at its viewing angle. Include off-axis views, bright windows, direct sunlight where applicable, and night operation. A dark laboratory can hide the problem that bonding is intended to solve.
Inspect image sharpness, haze, color shift, sparkle, reflections, and uniformity. Coatings on the outer glass remain important; bonding cannot remove reflection at the exposed surface.
Use the sunlight-readable display guide when the product operates outdoors. It treats optical performance and thermal load together.
Understand liquid and film processes
Bonding processes may use liquid optically clear adhesive or optically clear adhesive film. The right process depends on size, stack geometry, materials, equipment, and supplier experience.
Liquid processes need control of dispensing, flow, curing, bubbles, edge leakage, and shrinkage. Film processes need control of lamination, pressure, cleanliness, alignment, and trapped air.
Avoid choosing a process solely from a generic advantages list. Ask the supplier for demonstrated yield on a similar panel size and stack, defect definitions, rework method, and environmental qualification.
Request samples from normal production equipment. A hand-built engineering sample can look excellent while saying little about factory repeatability.
Include stress and thermal expansion
Glass, adhesive, touch layers, LCD structures, and the enclosure expand differently. Temperature cycles can create stress, edge separation, optical distortion, or pressure marks.
The mechanical design must avoid forcing the bonded assembly into a distorted bezel. Specify flatness, gasket compression, mounting torque, and allowable panel movement.
For air-gap designs, control the minimum gap across tolerances and loading. Touch pressure, vibration, or enclosure flex must not let the cover contact the LCD and create visible marks.
Neither architecture excuses weak mechanical support. Test the assembled product under the actual mounting method, including wall brackets or vehicle fixtures.
Treat touch tuning as part of the change
Bonding changes the dielectric stack seen by a capacitive touch sensor. Cover thickness, adhesive, grounding, and display noise can affect sensitivity and false-touch behavior.
Retune and validate the touch controller after the stack changes. Test dry fingers, gloves where supported, water, charger noise, and maximum backlight operation.
Check the corners and edges, where mechanical stress and grounding often differ. A successful center-screen tap test misses many integration failures.
The touchscreen integration guide provides the electrical and software checks that should accompany optical evaluation.
Define visible defects before buying volume
Create a shared inspection standard with lighting, distance, viewing angle, background patterns, and defect size or location limits. Without those conditions, the supplier and customer can disagree about every small bubble.
Distinguish cosmetic defects from functional risks. An edge bubble may be visually acceptable today but indicate adhesion that will worsen after temperature cycling.
Inspect alignment, bubbles, particles, adhesive overflow, edge sealing, mura, polarizer damage, and touch performance. Use traceable images for rejected samples.
| Inspection item | Initial check | Aging check |
|---|---|---|
| Bubbles and voids | Size, location, count | Growth after temperature and humidity |
| Particles | Visibility on defined patterns | No new contamination path |
| Edge adhesion | Continuous bonded boundary | No progressive separation |
| Image uniformity | White, gray, black patterns | No stress-related changes |
| Touch response | Grid and gesture test | Stable sensitivity after exposure |
| Seal integrity | Approved assembly method | Moisture resistance after cycling |
Model repair and yield costs
A bonded assembly can turn a cracked cover into replacement of the entire display module. That may be acceptable for a sealed outdoor product but expensive for a frequently damaged handheld terminal.
Ask whether damaged parts can be separated, what tools and solvents are required, and what yield the supplier achieves during rework. Do not count uncertain recovery value as guaranteed savings.
For air-gap assemblies, include the cost of dust control, gaskets, cleaning, mechanical spacers, and possible field condensation. Lower adhesive cost does not necessarily mean lower product cost.
Compare delivered assemblies at equivalent acceptance criteria. Include scrap, inspection time, transport protection, warranty returns, and service inventory.
Run a controlled comparison
Build otherwise identical air-gap and bonded samples where practical. Use the same LCD, backlight command, cover coating, application, and test conditions.
Measure optical performance and power, then perform mechanical and environmental tests appropriate to the product. Include multiple samples to see process variation.
Keep the comparison focused on product requirements. If the indoor installation already has adequate contrast and repairability is critical, bonding may provide little return. If outdoor readability is marginal, its optical benefit may avoid a much hotter backlight.
Document the decision and rejected alternatives. Future purchasing teams need to know why a cheaper stack is not automatically equivalent.
Frequently asked questions
Is optical bonding always better?
It often improves optical performance, but adds process and repair considerations. The better choice depends on ambient light, environmental requirements, volume yield, and service model.
Can an air gap cause condensation?
Yes, when moisture enters and surfaces cross the dew point. Enclosure sealing, venting strategy, temperature transitions, and material moisture must be evaluated.
Does bonding make the display impact-proof?
No. It changes load distribution, but cover strength, support geometry, adhesive properties, and the impact condition still determine the result.
Production handoff
Release the complete stack drawing, approved materials, bonding process revision, inspection standard, and environmental evidence together. Treat adhesive or coating substitutions as engineering changes. The EVT, DVT, and PVT guide helps place these decisions before tooling and production commitments.